Views: 0 Author: Site Editor Publish Time: 2026-09-28 Origin: Site


Steelmakers face intense pressure to cut Scope 1 and Scope 2 emissions while managing volatile industrial electricity rates. Melting scrap is inherently energy-intensive. Thermal losses, poor scrap mixes, and extended power-off times destroy operational efficiency. Suboptimal arc regulation extends tap-to-tap times and wastes megawatts of power. You need a structured approach to lower EAF energy consumption to protect profit margins. We will break down how to move from baseline audits to chemical and electrical optimizations. We cover practical methods for thermal loss mitigation. Finally, we evaluate advanced automation and heat recovery retrofits. This guide provides actionable steps to modernize your melt shop and stabilize your utility costs.
Baseline Measurement is Prerequisite: Effective energy reduction requires granular tracking of electrical vs. chemical energy inputs, alongside precise mapping of thermal losses (off-gas, cooling water, slag) and power-off delays.
Foamy Slag and Chemical Energy are Critical: Optimizing carbon and oxygen injection to maintain a robust foamy slag practice is the most cost-effective method to improve arc heat transfer and reduce electrical demand.
Minimizing Power-Off Time Saves Energy: Every minute the roof is open or power is off results in radiant heat loss; optimizing logistics to shorten tap-to-tap time directly lowers energy consumption per ton.
Automation Drives Consistency: Implementing closed-loop off-gas analysis and AI-driven electrode regulation eliminates operator-induced variability, yielding immediate energy savings with minimal downtime.
CAPEX vs. OPEX Trade-offs: High-impact structural changes, such as scrap preheating (e.g., shaft furnaces, Consteel), offer the highest energy reduction potential but require rigorous ROI and downtime evaluation compared to software-based process controls.
Table of Contents
You cannot optimize a process without measuring its inputs and outputs. The standard energy inputs for a modern furnace consist of electrical and chemical energy. Electrical energy typically provides 50 to 60 percent of the total input. Chemical energy makes up the remainder through oxy-fuel burners, oxygen lancing, and carbon oxidation. Exothermic reactions in the steel bath generate massive amounts of heat.
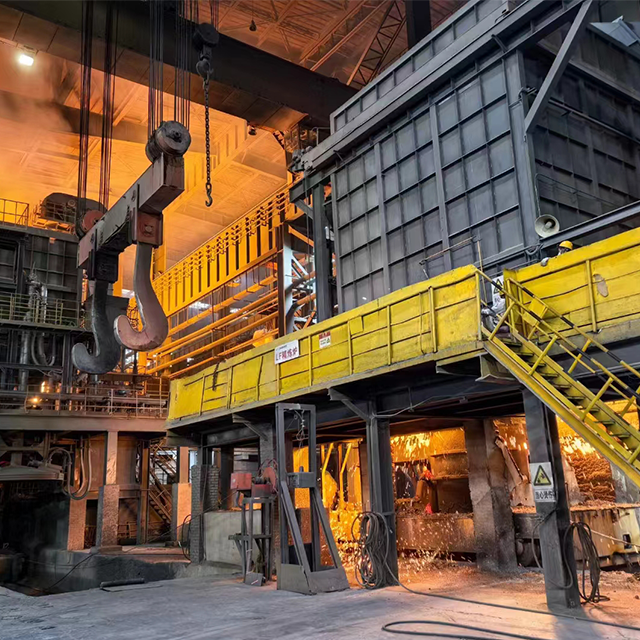
Energy outputs dictate your overall efficiency. Liquid steel represents the only useful energy output. The remaining energy exits the system as waste. Primary losses include thermal energy trapped in the liquid slag, hot off-gas exiting the fourth hole, and heat absorbed by the water-cooled panels. Radiant heat loss during power-off delays also drains the system continuously.
Energy Component | Typical Percentage (Input) | Typical Percentage (Output/Loss) |
|---|---|---|
Electrical Power | 50% - 60% | - |
Chemical Reactions (Burners, O2, Carbon) | 40% - 50% | - |
Liquid Steel (Useful Energy) | - | 50% - 55% |
Off-Gas Losses | - | 15% - 20% |
Cooling Water Losses | - | 10% - 15% |
Slag and Radiant Losses | - | 10% - 15% |
The industry-standard metric for measuring efficiency is kilowatt-hours per metric ton (kWh/t) of liquid steel. This metric provides a universal benchmark to compare different heats, shifts, and operating practices. Tracking this number daily highlights operational drift before it impacts the monthly utility bill.
Establish a plant-specific baseline using historical heat data. You must account for variables that skew the raw numbers. Adjust your baseline for target tap temperatures and raw material quality. Track the power-on versus power-off time ratio closely. A furnace running with a high utilization factor will always show lower specific energy consumption than one suffering from logistical delays.
Pull historical heat data for the last 90 days from your Level 2 system.
Filter out heats with abnormal delays, such as broken electrodes or hydraulic failures.
Calculate the average kWh/t for your standard scrap mixes.
Map the exact power-on and power-off minutes per heat to identify baseline utilization.
The way you stack scrap inside charging buckets affects arc stability and melting speed. Layer light scrap at the bucket bottom to protect hearth refractory, place heavy melting scrap in the center for the arc zone, and add medium scrap on top. Dirty scrap with rust, moisture and impurities absorbs heat and creates extra slag, raising power use and lengthening tap-to-tap cycles; clean, dense scrap blends deliver better energy performance.
Factories use DRI or HBI to lower harmful residual elements in steel. DRI contains acidic gangue that needs extra lime, which increases slag volume and consumes more electricity during melting. Still, continuous DRI feeding keeps the furnace roof closed and cuts radiant heat loss. Operators need to balance higher melting energy requirements against the energy savings from uninterrupted power-on operation.
Material Type | Impact on Slag Volume | Electrical Energy Demand | Operational Advantage |
|---|---|---|---|
Clean Shredded Scrap | Low | Baseline (Lowest) | Fast melting, low gangue |
Heavy Melting Scrap (HMS) | Low to Medium | Moderate | High yield, dense bath penetration |
Direct Reduced Iron (DRI) | High (due to gangue) | High (+20 to 40 kWh/t) | Continuous feeding, low residuals |
Hot Briquetted Iron (HBI) | Medium | Moderate to High | Dense, penetrates slag easily |
Modern hydraulic or electromechanical electrode regulation systems are mandatory for efficient operations. These systems maintain the optimal arc length by rapidly adjusting electrode positioning. Fast response times prevent short circuits when scrap shifts inside the shell. If the mast vibrates excessively, your regulation system is hunting and wasting power.
Minimizing arc voltage fluctuations reduces electrical losses across the secondary circuit. Stable arcs prevent excessive refractory wear and maximize active power input into the steel bath. Upgrading outdated proportional valves to high-speed servo valves yields immediate improvements in power transfer efficiency. The faster the hydraulic response, the tighter the arc control.

You must match transformer tap settings and reactor impedance to the specific melting stage. The bore-down phase requires different electrical parameters than the main melting or refining phases. Static power profiles waste energy and damage water-cooled panels. Operators should not manually guess the tap settings.
Modern operations shift toward high-voltage, long-arc profiles during the main melting phase. This maximizes active power input and speeds up the melting rate. You can only sustain long-arc operations if you maintain a robust foamy slag to shield the sidewalls from intense radiation. Without foamy slag, a long arc will melt your copper panels.
Preventative maintenance on the high-current secondary circuit is non-negotiable. The secondary circuit includes water-cooled cables, bus tubes, and electrode holders. Degradation in these components creates massive resistive heat losses. If your cables are hot to the touch, you are losing megawatts to the air.
Cleaning contact surfaces and torquing connections reduces resistive losses. Water-cooled cables degrade internally over time, increasing their electrical resistance. Replacing aged cables ensures more power reaches the arc. Inspect the delta closure regularly for arcing or loose connections. Clean the copper contact pads on the electrode arms to remove oxidation buildup.
Evaluate the return on investment for upgrading to ultra-high power (UHP) transformers. Pushing more active power into the furnace shortens the melting cycle and reduces time-dependent thermal losses. Faster heats consume less total energy because the furnace spends less time radiating heat to the atmosphere.
Implementing static VAR compensators (SVC) or STATCOMs improves the overall power factor. These systems stabilize the grid voltage and reduce flicker. A stable voltage supply allows the transformer to deliver maximum power continuously. This reduces grid penalties and lowers the specific energy consumption per ton.
Foamy slag is the foundation of modern furnace efficiency. Carbon reacts with iron oxide (FeO) in the slag to create carbon monoxide bubbles. These bubbles cause the slag to foam and expand, completely submerging the electric arc. A muffled arc sound indicates proper foaming. A loud, screaming arc means the arc is exposed.
Submerging the arc increases thermal transfer efficiency to the steel bath from roughly 40 percent to over 80 percent. It also shields the refractory and water-cooled panels from arc radiation. You must implement precise control of carbon and oxygen injection to sustain optimal slag volume throughout the entire power-on cycle. Keep the slag door clear of heavy buildup to allow proper slag flushing.
Transitioning from traditional oxy-fuel burners to coherent jet injectors transforms chemical energy utilization. Traditional burners lose gas velocity quickly, limiting their penetration into the scrap pile. Coherent jets surround the main oxygen stream with a flame envelope.
This envelope maintains supersonic gas velocity much deeper into the furnace. Coherent jets improve scrap cutting during the bore-down phase. They also enhance bath mixing and chemical energy transfer during the refining phase. Better mixing eliminates cold spots and reduces the total electrical demand required to reach tap temperature.
Carbon monoxide generated in the bath holds massive amounts of unreleased chemical energy. If this gas escapes to the fume extraction system, that energy is wasted. Injecting secondary oxygen above the bath converts carbon monoxide into carbon dioxide inside the furnace shell.
This exothermic reaction releases intense heat. Capturing this heat before it escapes to the off-gas system significantly lowers electrical demand. Proper post-combustion requires precise oxygen targeting to ensure the heat transfers to the scrap rather than damaging the exhaust ductwork. Monitor the temperature of your water-cooled ductwork to ensure combustion happens in the shell, not the exhaust.
Increasing oxygen injection lowers electrical energy consumption by driving exothermic reactions. You must balance this against the risk of iron oxidation. Pumping too much oxygen into the bath converts valuable liquid iron into iron oxide, which is lost to the slag.
This yield loss quickly negates the financial savings of reduced electricity usage. Implement a strict framework for oxygen lancing. Monitor slag chemistry to ensure iron oxide levels remain within acceptable limits. Chemical energy should supplement electrical power, not destroy metallic yield.
Real-time gas sensors and laser detectors monitor exhaust gas components from the furnace, tracking internal melting reactions instantly. The automatic system adjusts burner parameters and supplementary oxygen supply according to gas data. It burns unreacted carbon monoxide inside the furnace, recycles wasted chemical energy, and effectively improves overall melting efficiency.
AI melting systems analyze historical production data, real-time power parameters and exhaust gas conditions to accurately predict molten steel temperature and carbon content. This technology cancels frequent manual sampling and temperature testing, shortens heating time, avoids overheating, saves electricity consumption, and prolongs refractory service life.
AI intelligent systems may face compatibility and delay issues when matching old factory control equipment. Precise and clean sensor data is the core of accurate AI prediction. Regular sensor maintenance and daily lens cleaning are required; poor data quality will lead to invalid AI optimization and waste equipment investment.
Water-cooled panels and roof protect the furnace shell but continuously draw heat away from the molten bath. Adjust cooling water flow according to real panel temperature and fit RTD sensors on return pipes to track temperature difference; avoid running water pumps at full speed when panels stay cool. Apply zoned refractory design: place high-conductivity copper panels only in high-heat zones and use heavy-duty refractory on the lower furnace shell to hold heat inside, cutting the electricity needed to reach tapping temperature.
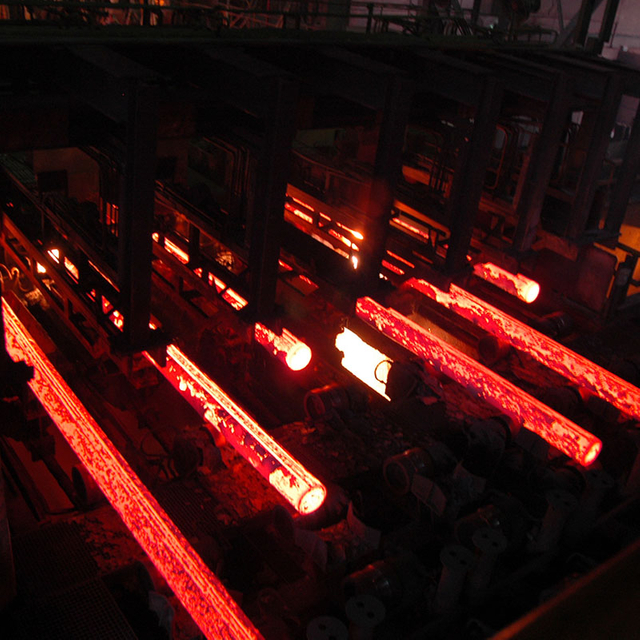
Scrap preheating delivers the largest cut in specific energy use by using hot furnace exhaust to warm scrap before melting. Shaft furnaces pass waste gas vertically through scrap piles, while Consteel systems continuously feed scrap on conveyors counter to hot gas flow. Though these technologies greatly reduce power consumption, they need large upfront investment, bring extra maintenance work and site layout limits, and require secondary combustion chambers to handle odor and VOC emissions.
Porous plugs fitted at the furnace hearth inject argon or nitrogen to stir molten steel. Inert gas mixing eliminates temperature layering, where the bath surface runs far hotter than the bottom. Uniform heat distribution lets operators lower the target tapping temperature; even a 10-degree reduction saves plenty of electricity and extends refractory service life.
There is a direct correlation between extended power-off times and radiant heat loss. Every minute the roof swings open for charging, the furnace loses thermal energy to the atmosphere. Electrode slipping, refractory patching, and tapping delays all extend the heat cycle.
Provide logistical strategies to streamline crane operations. The scrap yard must stage buckets perfectly to match the melting rhythm. The EAF should be constantly melting, not waiting on raw materials. If the ladle furnace is not ready to receive the heat, the melting furnace sits idle and loses temperature. Reducing power-off delays is the cheapest and fastest way to lower your energy consumption per ton.
Commission a comprehensive, third-party energy balance audit to identify specific thermal losses and establish a data-driven baseline.
Standardize scrap bucket loading procedures to ensure consistent density and minimize initial melting delays.
Upgrade electrode regulation valves and implement dynamic power profiling to maximize active power input.
Install closed-loop off-gas analysis to dynamically adjust burner ratios and recapture post-combustion heat.
Implement strict logistical tracking to eliminate crane delays and minimize power-off time during roof swings.
A: Modern furnaces typically consume between 350 and 450 kWh per metric ton of liquid steel. This variance depends heavily on the scrap mix, the utilization of chemical energy, and the efficiency of the foamy slag practice. Older furnaces or those experiencing frequent logistical delays may exceed 500 kWh/t.
A: Scrap preheating systems route hot exhaust gases from the furnace through incoming raw materials. This transfers waste heat into the cold scrap before it enters the shell. By pre-loading the scrap with thermal energy, the furnace requires significantly less electrical power to reach the final melting temperature.
A: Foamy slag submerges the electric arc, shielding the water-cooled panels and refractory from intense radiation. This forces the arc's thermal energy directly into the steel bath. Efficient heat transfer drastically reduces electrical power requirements and shortens the overall melting cycle.
A: Automation can reduce energy consumption by 2 to 5 percent per heat. Predictive melting software eliminates unnecessary power-off delays for manual temperature sampling. Closed-loop controls ensure optimal burner efficiency and prevent over-heating, yielding consistent energy savings across thousands of heats.
A: Electrical energy is supplied by the grid through the transformer and electrodes to create the melting arc. Chemical energy is generated inside the furnace through the combustion of natural gas in burners, the oxidation of carbon, and exothermic reactions driven by oxygen lancing.
A: Using Direct Reduced Iron generally increases electrical power consumption. DRI contains acidic gangue that requires more lime to neutralize, increasing the total slag volume. Melting this additional slag demands more energy, though continuous feeding systems offset some losses by keeping the roof closed.
A: Off-gas analysis measures the exact chemical composition of the exhaust exiting the furnace. By detecting unburned carbon monoxide, the automation system can dynamically inject secondary oxygen to burn the gas inside the shell. This recaptures exothermic heat that would otherwise be wasted in the ductwork.